<script type="text/javascript">
(function(a,l,b,c,r,s){_nQc=c,r=a.createElement(l),s=a.getElementsByTagName(l)[0];r.async=1;r.src=l.src=("https:"==a.location.protocol?"https://":"http://")+b;s.parentNode.insertBefore(r,s);})(document,"script","serve.albacross.com/track.js","89861715");
</script>
<script type="text/javascript">
var leady_track_key="Jt85ZWh81xgcWftq";
(function(){var l=document.createElement("script");l.type="text/javascript";l.async=true;l.src='https://t.leady.com/'+leady_track_key+"/L.js";var s=document.getElementsByTagName("script")[0];s.parentNode.insertBefore(l,s);})();
</script>
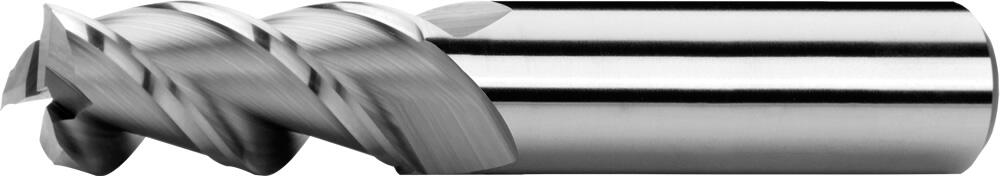
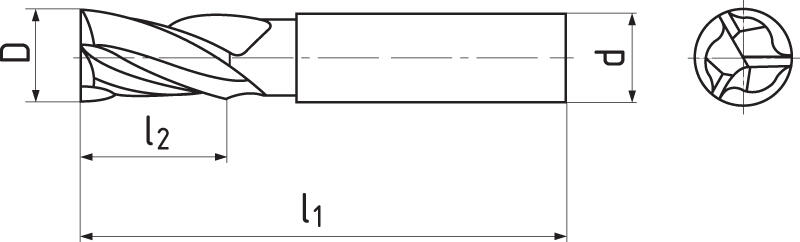
Home Catalogue End mills long, 1 tooth cut over centre, 45°, typ W, plain shank, code S111402, diameter 6 mm S111402.060 Solid carbide (SC) D d l1 l2 Z Item code On stock 6 6 57 13 3 S111402.060 Yes
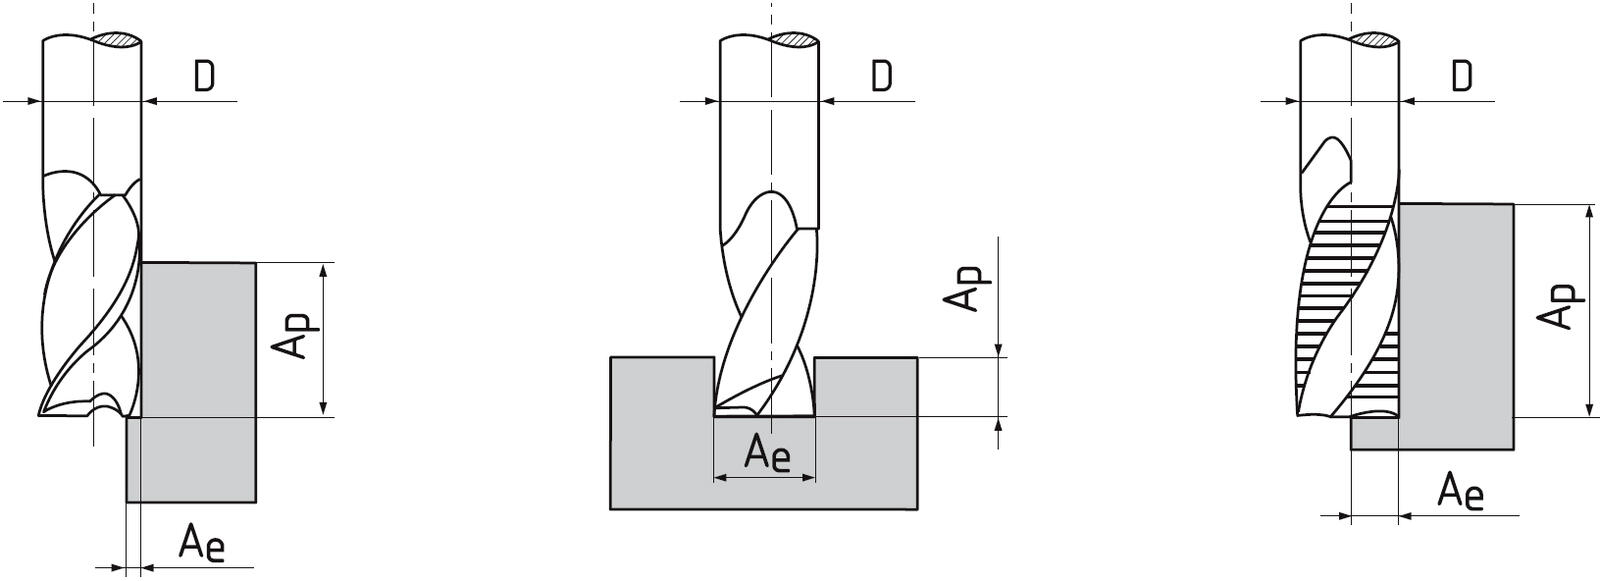
Cutting conditions p e c fz (mm/z) Ø 3Ø 6Ø 8Ø 10Ø 12Ø 16Ø 18Ø 20N.1 | Aluminium, Aluminium cast alloys Si (Si ≤ 6%) ≤ 400 N/mm2 1,5xD 0,2xD 160 0.02 0.04 0.053 0.067 0.08 0.107 0.13 0.135 N.2 | Aluminium cast alloys Si (Si ≤ 12%) ≤ 600 N/mm2 1,5xD 0,2xD 220 0.02 0.04 0.053 0.067 0.08 0.107 0.13 0.135 N.4 | Cooper-zinc alloys, cooper-tin alloys ≤ 800 N/mm2 1,5xD 0,2xD 176 0.016 0.032 0.0424 0.0536 0.064 0.0856 0.096 0.164
Calculations of cutting conditions
Product attributes Plain straight shank according to DIN 6535 HA.
For machining of soft materials, for example aluminium and non-ferrous metals.
Feed direction possibility Oil coolant. Company norm Helix angle = 45°. Rake angle = 15°.
End face design Carbide materials are characterised by high compressive strength, high hardness and therefore high wear resistance, but also limited flexural strength and toughness.
2026 © ZPS-FN a.s. | All right reserved